

TASARIMDAN İMALATA
Machining Operation Sequence
Plan datum faces, roughing, holes, finishing and threading around the requirements of the milled component.
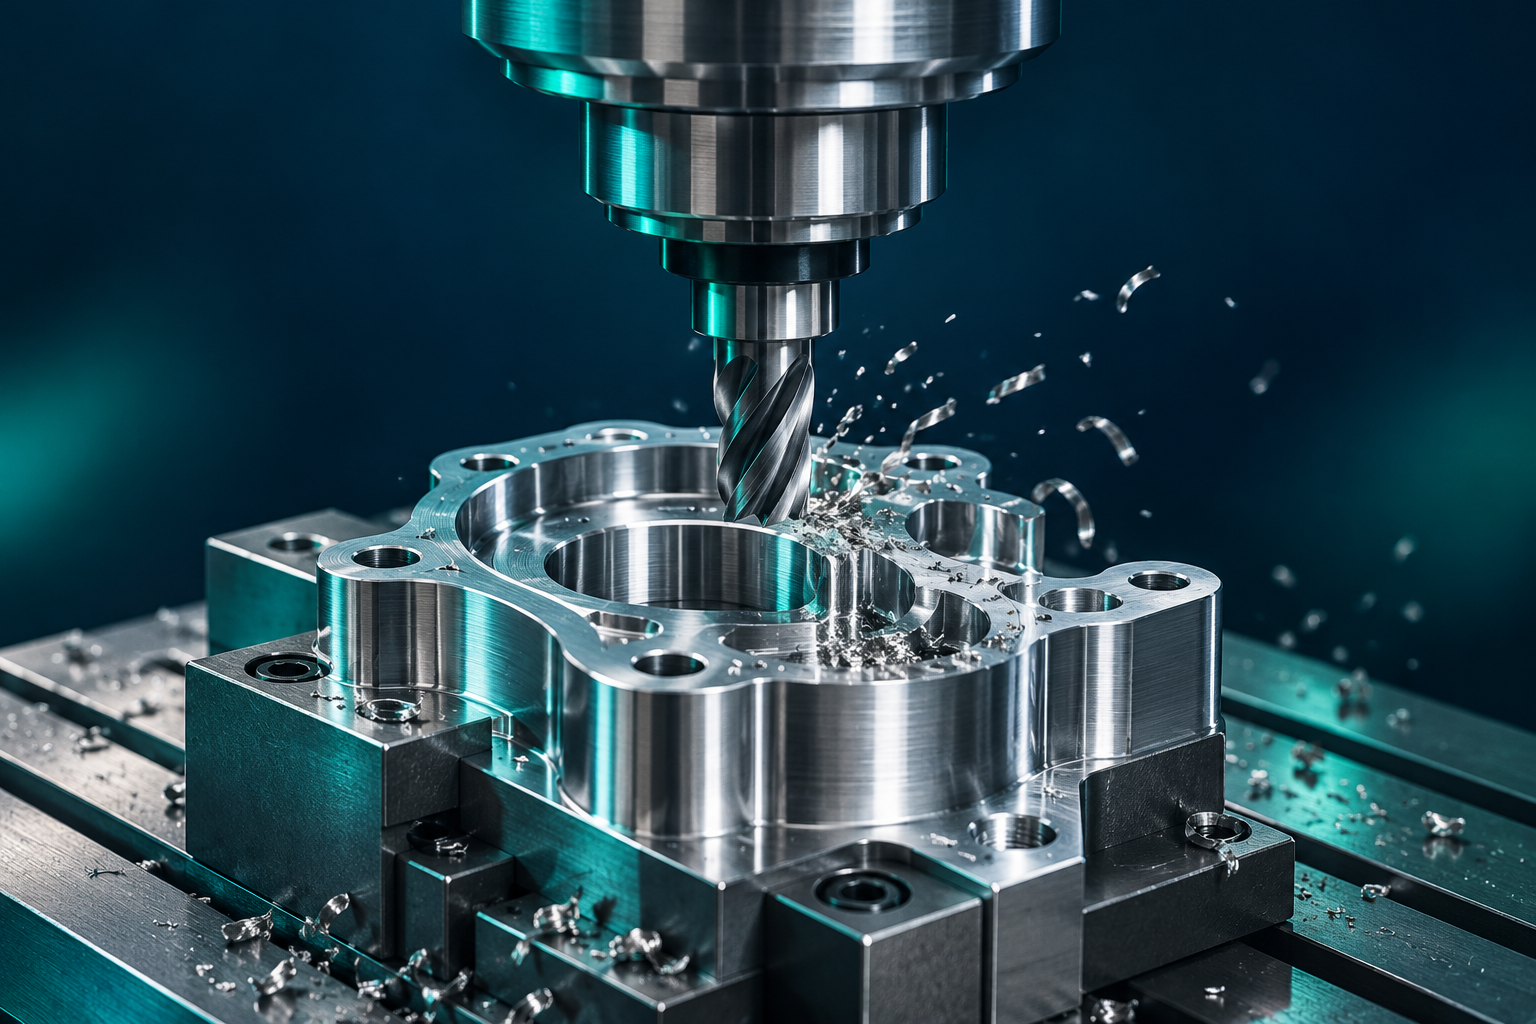
The part determines the sequence
There is no universal tool order. Assess the drawing, datums, tolerances, material, workholding and tool access together. Keep the component rigid, establish the required references and protect finished surfaces from later operations.
1. Datums and surface preparation
Check stock size, distortion and machining allowance; a mandatory 2 mm allowance does not apply to every part. Machine locating and measuring references first where necessary. Plan opposing face allowances and final thickness together.
2. Roughing and entry method
Rough pockets and contours with suitable finishing allowance. Choose a pre-drilled entry, helical entry or ramp according to tool capability, clearance and material. Drilling need not always precede end milling. Avoid removing support for thin walls prematurely.
3. Hole preparation
Spotting requirements depend on the drill manufacturer's guidance. Centre drills and spotting drills serve different purposes; check point angles and entry conditions. Allow for drill-point length, chip evacuation and bottom clearance in blind holes.
4. Precision surfaces and holes
Follow roughing with semi-finishing where needed, then finishing. Apply boring, reaming or burnishing with the appropriate pre-machined size and allowance. Select speed and feed from tool, material, runout and surface requirements, rather than a roughing/finishing label alone.
5. Chamfers, threads and burrs
The entry chamfer of a threaded hole is usually prepared before threading; use drawing requirements for its size and depth. Verify the pre-hole and chip space for tapping or thread milling. Threading does not always have to be last; consider subsequent operations.
6. Verification and inspection
Check workholding, work offsets, tool lengths and holder clearances. Inspect the first component after CAM checks and machine-specific NC verification. Include intermediate checks for critical dimensions, final deburring and acceptance in the plan.